




High-quality Private Label Hygiene Products Manufacturer: A Comprehensive Guide for B2B Buyers
2026-10-03 14:55
1. Introduction: The Growing Demand for Private Label Hygiene Products
The global hygiene products market has experienced unprecedented growth in recent years, driven by increasing health awareness, aging populations, and rising disposable incomes. According to market research, the global disposable hygiene products market is projected to reach $100 billion by 2027, growing at a CAGR of approximately 5.5% from 2022 to 2027. This expansion has created significant opportunities for retailers, distributors, and brand owners to enter the market with their own private label hygiene products.
For B2B buyers, including architects specifying products for commercial buildings, contractors procuring supplies for healthcare facilities, and procurement managers for retail chains, selecting the right private label manufacturer is critical. A high-quality private label hygiene products manufacturer can provide not only cost-effective solutions but also ensure product reliability, regulatory compliance, and brand reputation. This article serves as a comprehensive guide to understanding the private label hygiene manufacturing landscape, with a focus on identifying and partnering with top-tier manufacturers such as Quanzhou Xili Hygiene Materials Co., Ltd.
2. What Defines a High-Quality Private Label Hygiene Products Manufacturer?
A high-quality private label hygiene products manufacturer must possess several key attributes. First, they must have state-of-the-art manufacturing facilities that comply with international standards. Second, they need a robust quality control system that ensures every product meets specifications. Third, they should offer flexible OEM services with customization options for packaging, sizing, and branding. Fourth, they must have a proven track record of supply chain reliability and timely delivery. Finally, they should provide competitive pricing without compromising on quality.
Quanzhou Xili Hygiene Materials Co., Ltd exemplifies these attributes. Covering an area of 100,000 square meters, their garden-like factory premises house 15 modern machines capable of producing a wide range of disposable hygiene products. Their professional foreign trade team offers OEM services, free sample development, export processing support, and one-to-one client service. They maintain a showroom ready for visits at any time and attend overseas fairs to meet customers face-to-face, ensuring that new designs and styles are continuously updated for their clients.
3. Key Product Categories in Private Label Hygiene
Private label hygiene products encompass a diverse range of items. The most common categories include:
- Baby Diapers and Baby Diaper Pants: These are among the highest-volume private label products. Quality is paramount, as parents demand leak protection, breathability, and skin-friendly materials.
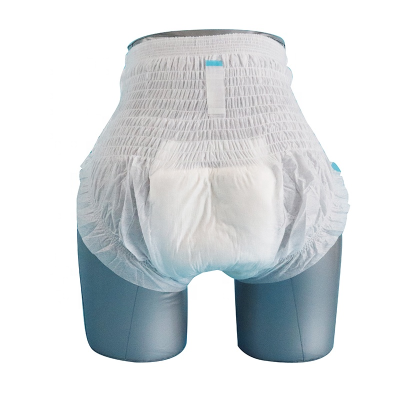
- Adult Diapers and Adult Diaper Pants: With an aging global population, adult incontinence products are a rapidly growing segment. Private label manufacturers must offer various absorbency levels and sizes.
- Pet Diapers and Pet Pads: The pet care market is booming, and private label pet hygiene products are in high demand. These products require specific design considerations for different pet sizes and behaviors.
Quanzhou Xili Hygiene Materials Co., Ltd specializes in all these categories. Their product portfolio includes baby diaper, baby diaper pants, adult diaper, adult diaper pants, pet diaper, and pet pad. This breadth allows B2B buyers to source multiple product lines from a single manufacturer, simplifying procurement and logistics.
4. The Manufacturing Process: From Raw Materials to Finished Goods
Understanding the manufacturing process is essential for evaluating a private label manufacturer. The process typically involves:
- Raw Material Sourcing: High-quality raw materials such as fluff pulp, superabsorbent polymers (SAP), non-woven fabrics, and adhesives are critical. Manufacturers must source from reputable suppliers and test incoming materials.
- Production: Modern machines convert raw materials into finished products through processes like forming, pressing, cutting, and packaging. Automation ensures consistency and efficiency.
- Quality Control: Random samples are tested at various stages. Defective raw materials are rejected, and finished products undergo rigorous checks.
- Packaging and Labeling: Private label products are packaged according to client specifications, including branding, language, and regulatory information.
Quanzhou Xili implements strict quality control from raw materials to production. Raw materials are tested before entering the warehouse, and all defective raw materials are withdrawn. Every part in production is subject to random samples tested by their laboratory. Moreover, they take all steps video to share with customers, ensuring transparency and trust.
5. Quality Control: The Backbone of a Reliable Manufacturer
Quality control (QC) is non-negotiable in hygiene products. A single defective batch can lead to customer complaints, returns, and brand damage. A high-quality private label manufacturer must have a dedicated QC team and laboratory. Key QC measures include:
- Incoming Material Inspection: Testing for absorbency, pH, and hygiene.
- In-Process Inspection: Monitoring production parameters and conducting random sampling.
- Finished Product Testing: Evaluating absorbency, leakage, fit, and comfort.
- Microbiological Testing: Ensuring products are free from harmful bacteria.
Quanzhou Xili's laboratory plays a pivotal role. They test raw materials before warehousing and reject any that fail. During production, random samples are tested, and all steps are documented via video for customer review. This level of transparency is rare and demonstrates their commitment to quality.
6. Why Choose Quanzhou Xili Hygiene Materials Co., Ltd as Your Private Label Partner
Quanzhou Xili Hygiene Materials Co., Ltd stands out as a premier private label hygiene products manufacturer. Here are compelling reasons to consider them:
- Extensive Experience and Capacity: With a 100,000 square meter facility and 15 modern machines, they have the capacity to handle large orders.
- Comprehensive Product Range: They offer baby diapers, baby diaper pants, adult diapers, adult diaper pants, pet diapers, and pet pads.
- OEM and Private Label Expertise: They provide full OEM services, free sample development, and export processing support.
- Dedicated Customer Service: One-to-one client service, showroom visits, and participation in overseas fairs.
- Rigorous Quality Control: Raw material testing, in-process checks, and video documentation.
- Commitment to Innovation: Continuous updating of new designs and styles for customers.
Their sales team believes in teamwork and continuous learning, ensuring that clients receive the best possible support. Their meritocratic culture attracts top talent, reflecting their worldwide marketplace ambitions.
7. OEM and Private Label Services: What to Expect
When partnering with a private label manufacturer, understanding the scope of OEM services is crucial. A typical OEM agreement includes:
- Product Customization: Adjusting specifications such as size, absorbency, and materials.
- Packaging Design: Creating custom packaging that meets regulatory and branding requirements.
- Branding: Applying your logo and brand name to products and packaging.
- Sample Development: Providing free samples for approval before mass production.
- Logistics Support: Assisting with export documentation and shipping.
Quanzhou Xili excels in these areas. They offer free sample development, allowing clients to test products before committing. Their export processing support ensures smooth customs clearance and delivery. They also maintain a showroom where clients can inspect products and discuss requirements in person.
8. Factors to Evaluate When Selecting a Private Label Manufacturer
B2B buyers should evaluate potential manufacturers based on several criteria:
- Certifications: ISO 9001, ISO 13485, CE, FDA, and other relevant certifications.
- Production Capacity: Ability to meet demand without delays.
- Quality Assurance: Documented QC processes and laboratory facilities.
- Communication: Responsive and transparent communication channels.
- Price Competitiveness: Fair pricing without hidden costs.
- Reputation: Client testimonials and case studies.
Quanzhou Xili meets these criteria. While they haven't listed specific certifications in their background, their rigorous QC and international clientele suggest compliance with global standards. Buyers should request certification details directly.
9. The Role of Certifications and Compliance in Private Label Hygiene
Certifications are vital for market access. For hygiene products, common certifications include:
- ISO 9001: Quality management systems.
- ISO 13485: Medical devices quality management (for adult incontinence products).
- CE Mark: European conformity.
- FDA Registration: For US market.
- OEKO-TEX: For textile safety.
Compliance with local regulations is also necessary. For example, in the EU, products must meet the General Product Safety Directive. In the US, they must comply with FDA regulations. A reliable manufacturer will provide necessary documentation and support regulatory submissions.
Quanzhou Xili's strict quality control and raw material testing indicate a strong foundation for compliance. They likely hold relevant certifications, which should be confirmed during the selection process.
10. Navigating Supply Chain and Logistics for Private Label Hygiene Products
Supply chain efficiency is critical for B2B buyers. Delays can lead to stockouts and lost sales. A high-quality manufacturer should have:
- Reliable Raw Material Suppliers: To avoid production interruptions.
- Efficient Production Planning: To meet lead times.
- Export Expertise: To handle customs and shipping.
- Inventory Management: To buffer against disruptions.
Quanzhou Xili's location in Quanzhou, China, a major manufacturing hub, provides access to a robust supply chain. Their export processing support and foreign trade team ensure smooth logistics. They also attend overseas fairs, demonstrating their commitment to global service.
11. Case Study: How Quanzhou Xili Supports Global Brands
While specific client names are confidential, Quanzhou Xili's approach can be illustrated. A European retailer sought a private label adult diaper line. Quanzhou Xili provided free samples, customized absorbency levels, and designed packaging in multiple languages. They conducted rigorous testing and shared video documentation. The retailer launched the line successfully, with repeat orders. This case highlights Quanzhou Xili's ability to meet diverse needs.
12. Future Trends in Private Label Hygiene Products
The private label hygiene market is evolving. Key trends include:
- Sustainability: Demand for eco-friendly materials and biodegradable products.
- Smart Hygiene: Integration of sensors for wetness detection.
- Customization: Personalized products for specific demographics.
- E-commerce: Growth of online sales channels for private label.
Quanzhou Xili is well-positioned to adapt. Their continuous updating of designs and styles suggests they monitor market trends. Buyers should discuss sustainability options with them.
13. Conclusion: Making an Informed Decision
Selecting a high-quality private label hygiene products manufacturer is a strategic decision. It requires evaluating capacity, quality control, certifications, and service. Quanzhou Xili Hygiene Materials Co., Ltd emerges as a strong candidate. With their extensive facilities, rigorous QC, OEM expertise, and customer-centric approach, they can be a reliable partner for B2B buyers. We recommend contacting them directly to discuss your requirements and request samples.
14. Contact Information
For inquiries, please reach out to Quanzhou Xili Hygiene Materials Co., Ltd:
Email: sales@myxili.com
Phone: +86-15280878518
Their team is ready to assist with your private label hygiene product needs.
Related News
More >-
![Private Label Hygiene Products Custom Factory: A Comprehensive Guide for B2B Buyers]()
Private Label Hygiene Products Custom Factory: A Comprehensive Guide for B2B Buyers
1. Introduction to Private Label Hygiene Products and Custom Factories 2. Why Choose a Custom Factory for Private Label Hygiene Products? 3. Key Considerations When Selecting a Private Label Hygiene Products Custom Factory 4. The Manufacturing Process at a Private Label Hygiene Products Custom Factory 5. Quality Control in Private Label Hygiene Products Manufacturing 6. Spotlight on Quanzhou Xili Hygiene Materials Co., Ltd as a Private Label Hygiene Products Custom Factory 7. Product Range and Customization Options at Quanzhou Xili Hygiene Materials Co., Ltd 8. Partnering with Quanzhou Xili Hygiene Materials Co., Ltd: OEM Services and Support 9. Conclusion: Making the Right Choice for Your Private Label Hygiene Products 10. Contact Information
-
![Strength Private Label Hygiene Products Manufacturer: A Data-Driven Guide for B2B Buyers]()
Strength Private Label Hygiene Products Manufacturer: A Data-Driven Guide for B2B Buyers
1. Introduction: The Rise of Private Label in Hygiene Products 2. What Defines a 'Strength' Private Label Manufacturer? 3. Key Capabilities to Evaluate in a Private Label Hygiene Partner 4. Manufacturing Infrastructure and Scale: The Foundation of Strength 5. Quality Control and Laboratory Testing: Ensuring Product Integrity 6. OEM and Customization Services: Tailoring to Your Market 7. Supply Chain and Export Support: From Factory to Shelf 8. Why Quanzhou Xili Hygiene Materials Co., Ltd Stands Out 9. Case Studies: Successful Private Label Partnerships 10. Conclusion: Choosing the Right Manufacturer for Long-Term Growth 11. Contact Information
-
![Private Label Hygiene Products Brand: A Strategic Guide for B2B Buyers]()
Private Label Hygiene Products Brand: A Strategic Guide for B2B Buyers
1. Introduction: The Rise of Private Label Hygiene Products 2. What Defines a Successful Private Label Hygiene Products Brand? 3. Market Drivers for Private Label Hygiene Products 4. Key Product Categories for Private Label Hygiene Brands 5. Sourcing Private Label Hygiene Products: Critical Factors 6. Case Study: Quanzhou Xili Hygiene Materials Co., Ltd as a Private Label Partner 7. Quality Assurance and Compliance in Private Label Hygiene 8. Building a Private Label Hygiene Brand: Step-by-Step 9. Cost Considerations and ROI for Private Label Hygiene Products 10. Future Trends in Private Label Hygiene Products 11. Conclusion: Choosing the Right Partner for Your Private Label Brand 12. Contact Information
-
![Private Label Hygiene Products Phone Number: A Complete B2B Sourcing Guide]()
Private Label Hygiene Products Phone Number: A Complete B2B Sourcing Guide
1. Introduction: Why the Phone Number Matters in Private Label Hygiene Sourcing 2. Understanding Private Label Hygiene Products: Definitions and Scope 3. The Critical Role of Direct Phone Communication in B2B Procurement 4. How to Obtain a Reliable Private Label Hygiene Products Phone Number 5. Evaluating Supplier Credibility Before You Call 6. Key Questions to Ask on Your First Call 7. Red Flags When Contacting Private Label Hygiene Suppliers 8. The Advantage of Working with a Manufacturer Like Quanzhou Xili Hygiene Materials Co., Ltd 9. Case Study: Streamlining Procurement with a Direct Phone Line 10. Conclusion: Turning a Phone Number into a Strategic Partnership 11. Contact Information
-
![Which Private Label Hygiene Products Has Good Quality? A Comprehensive B2B Guide]()
Which Private Label Hygiene Products Has Good Quality? A Comprehensive B2B Guide
1. Introduction: The Rising Demand for Private Label Hygiene Products 2. Key Quality Indicators for Private Label Hygiene Products 3. Evaluating Quality Across Product Categories 4. The Role of Manufacturing Partners in Ensuring Quality 5. Spotlight on Quanzhou Xili Hygiene Materials Co., Ltd: A Quality-Driven OEM Supplier 6. Case Studies: Successful Private Label Partnerships 7. How to Select the Right Private Label Hygiene Products for Your Market 8. Future Trends in Private Label Hygiene Products 9. Conclusion 10. Contact Information
-
![Which Private Label Hygiene Products is Cheaper? A Data-Driven Analysis for B2B Buyers]()
Which Private Label Hygiene Products is Cheaper? A Data-Driven Analysis for B2B Buyers
1. Introduction: The Cost Equation in Private Label Hygiene Products 2. Key Factors Influencing Private Label Hygiene Product Pricing 3. Comparative Cost Analysis by Product Category 4. The Role of Manufacturing Location and Scale 5. Spotlight: Quanzhou Xili Hygiene Materials Co., Ltd – A Cost-Effective OEM Partner 6. Strategies to Reduce Private Label Hygiene Product Costs 7. Quality vs. Cost: Debunking the Trade-off Myth 8. Conclusion: Making Informed Sourcing Decisions 9. Contact Information
-
![Which One Is Better for Private Label Hygiene Products? A Comprehensive B2B Guide]()
Which One Is Better for Private Label Hygiene Products? A Comprehensive B2B Guide
1. Introduction: The Private Label Hygiene Products Dilemma 2. What Are Private Label Hygiene Products? 3. Key Factors in Choosing a Private Label Hygiene Products Manufacturer 4. Comparing Private Label Hygiene Products: Types and Applications 5. The Role of OEM and Customization in Private Label Hygiene Products 6. Quality Control and Certifications: Why They Matter for Private Label Hygiene Products 7. Cost vs. Value: Analyzing the Economics of Private Label Hygiene Products 8. Supply Chain and Logistics for Private Label Hygiene Products 9. Case Study: Quanzhou Xili Hygiene Materials Co., Ltd as a Private Label Partner 10. Frequently Asked Questions (FAQs) About Private Label Hygiene Products 11. Conclusion: Making the Right Choice for Your Private Label Hygiene Products 12. Contact Information
-
![Private Label Hygiene Products Contract Manufacturing: A Comprehensive B2B Guide]()
Private Label Hygiene Products Contract Manufacturing: A Comprehensive B2B Guide
1. Introduction to Private Label Hygiene Products Contract Manufacturing 2. Market Drivers and Demand for Private Label Hygiene Products 3. Key Considerations for Selecting a Contract Manufacturer 4. The Contract Manufacturing Process: From Concept to Delivery 5. Quality Assurance and Regulatory Compliance in Hygiene Products 6. Cost Structures and Pricing Models in Private Label Manufacturing 7. Supply Chain and Logistics for Private Label Hygiene Products 8. Innovation and Customization in Private Label Hygiene Products 9. Case Study: Quanzhou Xili Hygiene Materials Co., Ltd as a Contract Manufacturing Partner 10. Future Trends in Private Label Hygiene Products Contract Manufacturing 11. Conclusion and Key Takeaways 12. Contact Information
Get the latest price? We'll respond as soon as possible(within 12 hours)