





Private Label Hygiene Products Manufacturing Plant: A Comprehensive Guide for B2B Buyers
2026-10-01 14:54
Introduction to Private Label Hygiene Products Manufacturing
In the competitive landscape of disposable hygiene products, private label manufacturing has emerged as a strategic avenue for retailers, distributors, and brands seeking to offer high-quality products under their own labels. A private label hygiene products manufacturing plant specializes in producing goods such as baby diapers, adult diapers, pet diapers, and related items that are sold under the buyer's brand name. This model allows businesses to bypass the complexities of owning production facilities while maintaining control over branding, marketing, and customer relationships. For B2B buyers—including architects specifying facilities, contractors involved in plant setup, and procurement managers sourcing products—understanding the nuances of private label manufacturing is crucial. This article provides an in-depth, data-driven guide to private label hygiene products manufacturing plants, with a focus on key factors, processes, and a spotlight on Quanzhou Xili Hygiene Materials Co., Ltd, a leading supplier in this sector.
Key Considerations When Selecting a Manufacturing Plant
Choosing the right manufacturing partner is critical to the success of a private label hygiene products line. Several factors must be evaluated to ensure alignment with business goals, quality standards, and market demands.
Production Capacity and Scalability
A plant's capacity determines its ability to meet current and future order volumes. Facilities with modern machinery and multiple production lines can handle large-scale orders efficiently. For instance, a plant covering 100,000 square meters with 15 modern machines can produce millions of units monthly, ensuring timely delivery even during peak seasons. Scalability is equally important; the partner should be able to ramp up production as your brand grows without compromising quality.
Quality Control and Certifications
Hygiene products are subject to stringent regulations regarding safety, absorbency, and materials. A reputable manufacturing plant implements rigorous quality control measures at every stage, from raw material inspection to final product testing. Certifications such as ISO 9001, CE, FDA, and others demonstrate compliance with international standards. Buyers should request documentation and audit reports to verify a plant's commitment to quality.
Customization and OEM Services
Private label manufacturing thrives on customization. The plant should offer OEM services, allowing buyers to specify product design, materials, packaging, and branding. Free sample development and design updates are valuable services that facilitate product differentiation. A plant with a professional foreign trade team and one-to-one client service can streamline communication and ensure specifications are met accurately.
Cost Efficiency and Lead Times
Cost competitiveness is a major driver for private label sourcing. Manufacturing plants in regions with optimized supply chains and labor costs can offer attractive pricing without sacrificing quality. However, buyers must also consider lead times—delays can disrupt market entry. A plant with a garden-like factory premises and efficient logistics can maintain short lead times, often shipping within 30-45 days after order confirmation.
Supplier Reputation and Experience
Experience in the hygiene industry is a strong indicator of reliability. A plant with years of operation, a diverse clientele, and a track record of successful partnerships is likely to be a stable partner. Visiting the facility, attending trade shows, and checking references are recommended due diligence steps.
The Manufacturing Process for Private Label Hygiene Products
Understanding the manufacturing process helps buyers appreciate the complexity and precision required in hygiene product production. The process typically involves several stages:
Raw Material Sourcing and Testing
High-quality raw materials are the foundation of superior hygiene products. Materials such as super absorbent polymers (SAP), fluff pulp, non-woven fabrics, and adhesives are sourced from reputable suppliers. At a well-managed plant, all raw materials undergo testing before entering the warehouse; defective materials are rejected. This pre-production quality check ensures consistency and safety.
Production Line Operations
Modern manufacturing plants utilize automated production lines for efficiency and precision. For diapers, the process includes forming the absorbent core, attaching leg cuffs, applying fasteners, and sealing edges. Each machine is calibrated to produce products that meet design specifications. In a facility with 15 modern machines, multiple product types (baby diapers, adult diapers, pet pads, etc.) can be produced simultaneously, optimizing output.
In-Process Quality Control
Quality control is not limited to the end of the line. Random samples are taken during production and tested in an on-site laboratory for parameters like absorbency, retention, pH, and tensile strength. This real-time monitoring allows immediate adjustments, reducing waste and ensuring that only compliant products proceed to packaging.
Packaging and Branding
For private label orders, packaging is customized to reflect the buyer's brand. This includes designing bags, boxes, and labels with the buyer's logo, product information, and marketing claims. The plant should have capabilities for various packaging formats, including poly bags, cartons, and display boxes.
Final Inspection and Shipping
Before shipment, finished products undergo final inspection to verify quantity, packaging integrity, and labeling accuracy. The plant then arranges logistics, often providing video documentation of the entire process to assure buyers of quality and compliance.
Quality Control and Certifications in Hygiene Manufacturing
Quality control is paramount in hygiene product manufacturing due to the sensitive nature of the products. A robust quality management system (QMS) encompasses:
Raw Material Testing: Every batch of raw materials is tested for purity, safety, and performance. Defective materials are rejected and returned to suppliers.
In-Process Testing: During production, samples are randomly selected and tested in the laboratory. Tests may include absorbency rate, rewet, leakage, and dimensional checks.
Finished Product Testing: Final products are tested for overall performance, including fit, comfort, and durability. Only products passing all tests are approved for sale.
Certifications: Leading plants hold certifications such as ISO 9001 (Quality Management), ISO 14001 (Environmental Management), CE (European Conformity), FDA (U.S. Food and Drug Administration) registration, and others relevant to target markets. These certifications are essential for market access and consumer trust.
Traceability: A good QMS includes traceability systems that track materials and processes, enabling quick identification and resolution of any issues.
Why Quanzhou Xili Hygiene Materials Co., Ltd Stands Out as a Private Label Partner
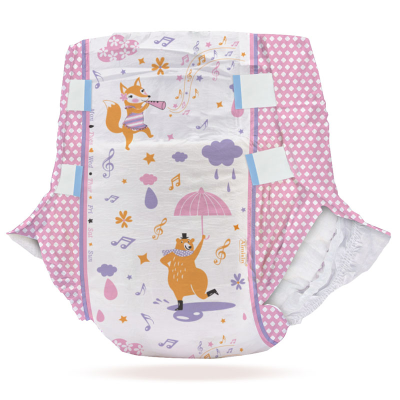
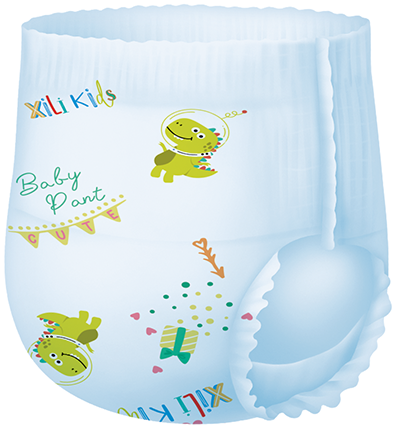
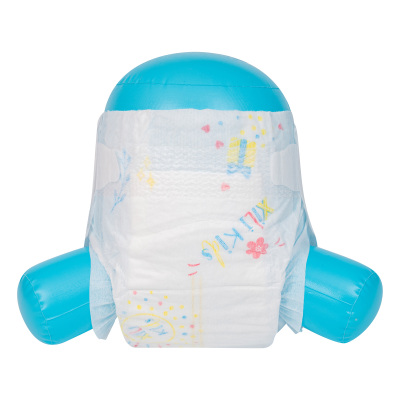
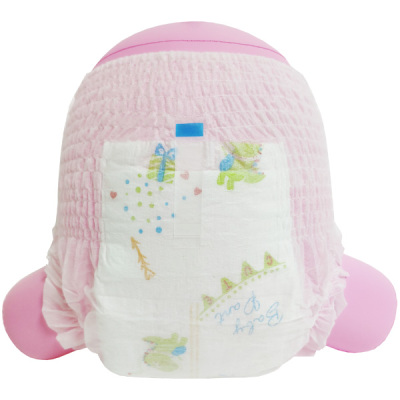
Quanzhou Xili Hygiene Materials Co., Ltd is a professional supplier of disposable hygiene products, including baby diapers, baby diaper pants, adult diapers, adult diaper pants, pet diapers, and pet pads. With a strong focus on OEM services and private label manufacturing, the company has established itself as a reliable partner for B2B clients worldwide.
Company Background and Facilities
Quanzhou Xili Hygiene Materials Co., Ltd operates from a garden-like factory premises covering an area of 100,000 square meters. The facility is equipped with 15 modern machines, enabling efficient production of a wide range of hygiene products. The company's professional foreign trade team provides comprehensive support, including OEM services, free sample development, export processing support, and one-to-one client service. A showroom is available for clients to visit at any time, and the company regularly attends overseas fairs to meet customers face-to-face. New designs and styles are continuously updated to keep pace with market trends.
Quality Control and Laboratory
Quality is at the core of Quanzhou Xili's operations. From raw materials to production, the company maintains strict quality control. Raw materials are tested before entering the warehouse, and all defective materials are withdrawn. During production, random samples are tested by the on-site laboratory. The company also takes videos of all steps to share with customers, ensuring transparency and trust.
Customer-Centric Approach
Quanzhou Xili believes in creating loyal customers by delivering superior products and excellent after-sales service. The sales team is committed to teamwork, continuous learning, and professional growth, reflecting the company's dedication to being a meritocracy in the global marketplace.
Product Range and Customization
The company offers a diverse range of products, including:
- Baby Diapers and Diaper Pants
- Adult Diapers and Diaper Pants
- Pet Diapers and Pet Pads
All products can be customized to meet specific buyer requirements, from materials and absorbency levels to packaging and branding. This flexibility makes Quanzhou Xili an ideal partner for private label initiatives.
Conclusion and Call to Action
Selecting the right private label hygiene products manufacturing plant is a strategic decision that impacts product quality, brand reputation, and market success. By considering factors such as production capacity, quality control, customization, and supplier reputation, B2B buyers can make informed choices. Quanzhou Xili Hygiene Materials Co., Ltd exemplifies a reliable, quality-focused manufacturing partner with extensive experience, modern facilities, and a customer-centric approach. For businesses looking to launch or expand their private label hygiene products line, partnering with a proven manufacturer like Quanzhou Xili can provide a competitive edge.
For inquiries, sample requests, or to discuss your private label project, please contact Quanzhou Xili Hygiene Materials Co., Ltd directly. Their team is ready to assist with tailored solutions.
Contact Information
Email: sales@myxili.com
Phone: +86-15280878518
Related News
More >-
![Which Baby Diaper Factory Is Good? A Comprehensive Guide for B2B Buyers]()
Which Baby Diaper Factory Is Good? A Comprehensive Guide for B2B Buyers
1. Introduction: The Importance of Choosing a Reliable Baby Diaper Factory 2. Key Factors to Evaluate a Baby Diaper Factory 3. Why Quanzhou Xili Hygiene Materials Co., Ltd. Stands Out 4. Product Range and Quality Assurance 5. OEM/ODM Services and Customization 6. Global Reach and Customer Support 7. Conclusion: Making the Right Choice 8. Contact Information
-
![Which Baby Diaper Company is Good? A B2B Buyer's Guide to Selecting a Reliable Supplier]()
Which Baby Diaper Company is Good? A B2B Buyer's Guide to Selecting a Reliable Supplier
1. Introduction: The Importance of Choosing the Right Baby Diaper Supplier
2. Key Factors in Evaluating a Baby Diaper Company
3. The Role of Certifications and Quality Standards
4. Product Range and Customization Capabilities
5. Supply Chain Reliability and Logistics
6. Cost-Effectiveness and Pricing Transparency
7. Spotlight on Quanzhou Xili Hygiene Materials Co., Ltd.
8. Conclusion: Making an Informed Decision
9. Contact Information
-
![Which Baby Diaper Supplier Is Good? A Comprehensive Guide for B2B Buyers]()
Which Baby Diaper Supplier Is Good? A Comprehensive Guide for B2B Buyers
1. Introduction
2. Key Factors to Evaluate a Baby Diaper Supplier
3. The Role of Certifications and Compliance
4. Product Quality and Performance Metrics
5. Supply Chain Reliability and Capacity
6. Cost Structure and Pricing Transparency
7. OEM/ODM Capabilities and Customization
8. Customer Support and Communication
9. Case Study: Quanzhou Xili Hygiene Materials Co., Ltd.
10. Conclusion
11. Contact Information
-
![Which Chinese Baby Diaper Manufacturer is Good? A Comprehensive Guide for B2B Buyers]()
Which Chinese Baby Diaper Manufacturer is Good? A Comprehensive Guide for B2B Buyers
1. Introduction: The Global Demand for Chinese Baby Diapers 2. Key Factors in Evaluating a Chinese Baby Diaper Manufacturer 3. Top Chinese Baby Diaper Manufacturers: An Overview 4. Spotlight on Quanzhou Xili Hygiene Materials Co., Ltd. 5. Comparing Manufacturers: What Sets Leaders Apart 6. The Importance of OEM/ODM Partnerships 7. Quality Assurance and Certifications 8. Supply Chain and Logistics Considerations 9. Pricing and Minimum Order Quantities 10. Sustainability and Ethical Practices 11. Case Studies: Successful Partnerships with Chinese Manufacturers 12. Conclusion: Making an Informed Decision 13. Contact Information
-
![Which Chinese Baby Diaper Factory is Good? A Comprehensive Guide for B2B Buyers]()
Which Chinese Baby Diaper Factory is Good? A Comprehensive Guide for B2B Buyers
1. Introduction: The Growing Demand for Quality Baby Diapers
2. Key Factors to Evaluate a Chinese Baby Diaper Factory
3. Top Chinese Baby Diaper Factories: An Overview
4. Spotlight on Quanzhou Xili Hygiene Materials Co., Ltd.
5. Comparing Quanzhou Xili with Other Leading Factories
6. How to Choose the Right Factory for Your Business
7. Conclusion: Making an Informed Decision
8. Contact Information
-
![Which Chinese Baby Diaper Company Is Good? A B2B Buyer's Guide to Sourcing from China]()
Which Chinese Baby Diaper Company Is Good? A B2B Buyer's Guide to Sourcing from China
Introduction
Key Criteria for Evaluating Chinese Baby Diaper Manufacturers
Top Chinese Baby Diaper Companies: An Overview
Quanzhou Xili Hygiene Materials Co., Ltd: A Trusted Partner for Global Buyers
Product Range and Specifications
Quality Assurance and Certifications
OEM/ODM Services and Customization
Supply Chain and Logistics
Minimum Order Quantities and Lead Times
Pricing and Cost Considerations
Case Studies and Client Testimonials
How to Choose the Right Partner
Conclusion
Contact Information
-
![Which Chinese Baby Diaper Supplier Is Good? A Data-Driven Evaluation for B2B Buyers]()
Which Chinese Baby Diaper Supplier Is Good? A Data-Driven Evaluation for B2B Buyers
1. Introduction: The Sourcing Challenge for Baby Diaper Buyers 2. Key Criteria for Evaluating a Chinese Baby Diaper Supplier 3. The Chinese Baby Diaper Manufacturing Landscape: Strengths and Challenges 4. Spotlight on Quanzhou Xili Hygiene Materials Co., Ltd. 5. Product Range and Quality Assurance 6. OEM/ODM Capabilities and Customization 7. Supply Chain and Logistics 8. Pricing and Minimum Order Quantities 9. Customer Support and Communication 10. Compliance and Certifications 11. Case Studies and Testimonials 12. How to Vet a Supplier: A Step-by-Step Checklist 13. Common Pitfalls and How to Avoid Them 14. Future Trends in Baby Diaper Sourcing 15. Conclusion and Recommendations 16. Contact Information
-
![What are the High-Quality Baby Diaper Manufacturers? A Comprehensive Guide for B2B Buyers]()
What are the High-Quality Baby Diaper Manufacturers? A Comprehensive Guide for B2B Buyers
1. Introduction: The Importance of Sourcing High-Quality Baby Diaper Manufacturers 2. Key Criteria for Evaluating Baby Diaper Manufacturers 3. Top High-Quality Baby Diaper Manufacturers: A Global Overview 4. Spotlight on Quanzhou Xili Hygiene Materials Co., Ltd.: A Trusted Partner for Global Buyers 5. How to Vet and Select the Right Baby Diaper Manufacturer 6. The Role of Certifications and Compliance in Ensuring Quality 7. Trends and Innovations in Baby Diaper Manufacturing 8. Conclusion: Making Informed Sourcing Decisions 9. Contact Information
Get the latest price? We'll respond as soon as possible(within 12 hours)